Description
1. Product Overview
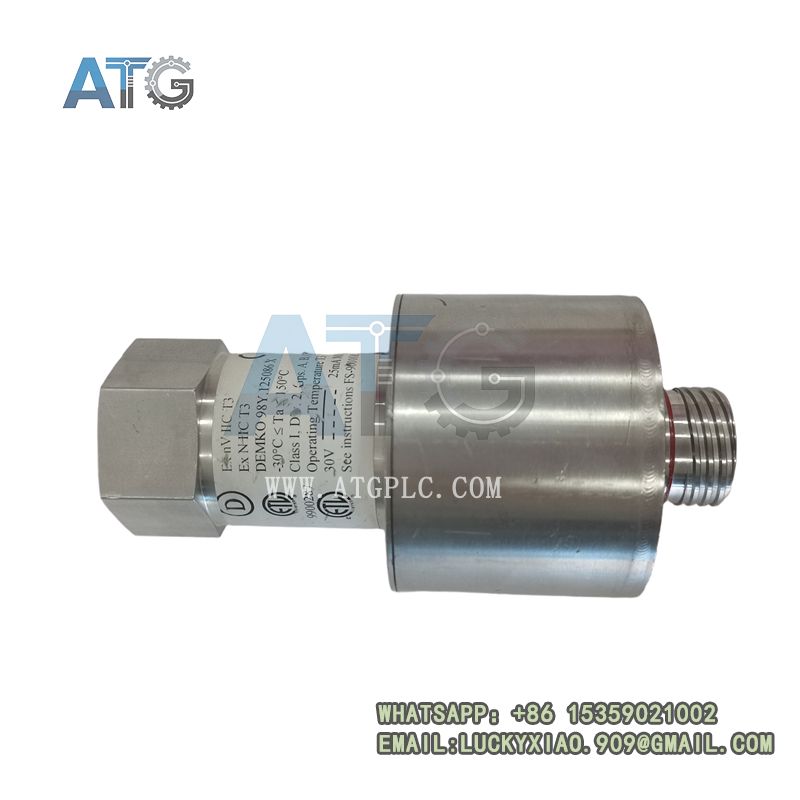
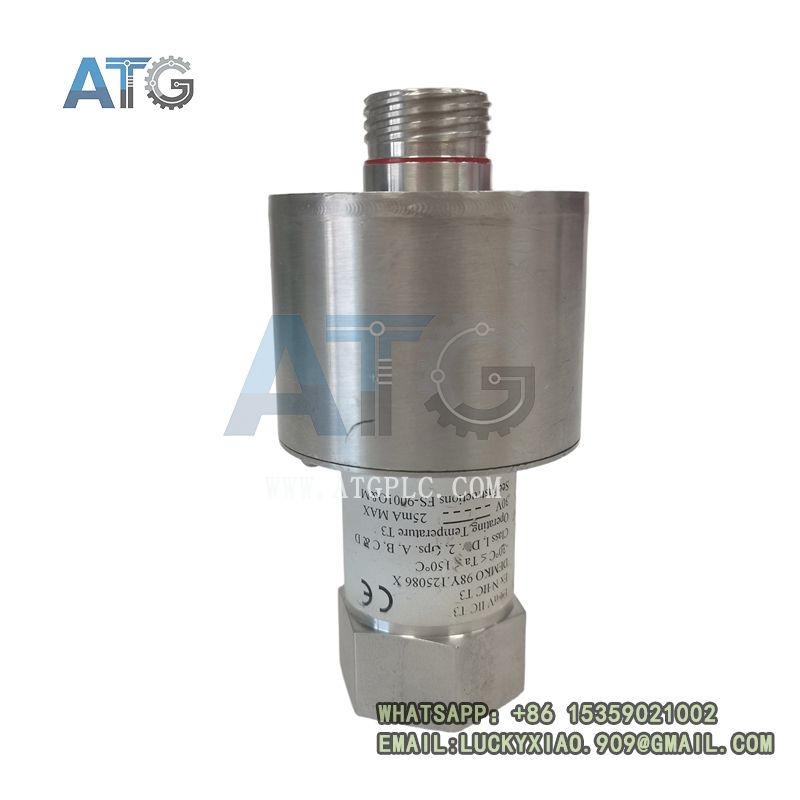
The GE RS-FS-9001 is a high-performance industrial UV flame detector developed for safety monitoring and fire prevention systems. Adopting professional silicon carbide (SiC) ultraviolet sensing technology, this device serves as a core flame monitoring probe for industrial combustion equipment. It accurately captures real-time flame signals, outputs standard analog signals and supports long-term stable online monitoring. It effectively identifies abnormal flame extinguishment, flame deviation and hidden fire risks. This detector is widely deployed in power generation plants, petrochemical facilities, industrial boilers and flammable and explosive industrial scenarios.
Traditional ordinary flame detectors have obvious application limitations in harsh industrial environments. Most conventional detectors adopt low-sensitivity sensing components. They feature slow response speed, narrow detection range and poor anti-interference capability. They are easily affected by ambient light, smoke and electromagnetic signals, resulting in false alarms or missed detection. In addition, ordinary probes have short service life and poor temperature resistance. They cannot adapt to long-term high-temperature and high-load industrial operation. In contrast, the GE RS-FS-9001 adopts industrial-grade SiC UV sensing chips and optimized signal filtering algorithms. It achieves ultra-fast response and high-precision flame identification. Each unit passes strict high-low temperature aging, vibration testing and full-function calibration before factory delivery. It has become a mainstream device for industrial flame monitoring system upgrading, old equipment replacement and global industrial e-commerce standardized procurement.
2. Core Product Features & Competitive Advantages
Industrial flame safety monitoring requires detection devices to deliver high sensitivity, fast response, strong anti-interference and ultra-high operational reliability. Ordinary civilian and low-grade industrial detectors cannot meet the strict safety monitoring standards of flammable and explosive scenarios. As a professional industrial flame detection probe, the GE RS-FS-9001 optimizes sensing performance, structural stability and environmental adaptability in all dimensions. It provides reliable safety guarantee for industrial combustion system operation.
-
Advanced SiC UV Sensing Technology: Equipped with high-precision silicon carbide ultraviolet sensor. It exclusively identifies effective flame UV spectral signals. It filters out ambient visible light, infrared interference and stray light noise. It greatly reduces false alarm and missing alarm rates.
-
Ultra-Fast Detection Response: Features ≤10ms ultra-short response time. It instantly captures flame state changes and abnormal extinguishment signals. It supports timely linkage of alarm and protection systems to avoid industrial safety accidents.
-
Long-Distance & Wide-Angle Detection: Supports up to 15-meter long-distance flame monitoring and 90° wide detection angle. It covers a large monitoring area. It meets the detection demands of large boiler combustion chambers and wide-range industrial combustion equipment.
-
Standard 4-20mA Analog Output: Matches universal industrial 4-20mA current loop signal output. The signal is proportional to flame intensity. It realizes real-time flame data transmission and accurate flame state judgment for upper control systems.
-
Two-Wire Simplified Wiring Design: Adopts convenient two-wire wiring mode. It simplifies on-site wiring construction and reduces engineering costs. It supports quick system docking and equipment debugging.
-
Ultra-High Operational Reliability: Features ultra-long MTBF with up to 500 million stable operating hours. It adopts integrated welded anti-disassembly structure. It avoids loose circuit failure and ensures long-term uninterrupted operation.
-
Excellent Harsh Environment Adaptability: Industrial-grade component selection and wide-temperature design support extreme temperature operation. It resists high temperature, low temperature, humidity, dust and industrial electromagnetic interference.
-
High-Level Ingress Protection: Reaches IP65/IP66 industrial dustproof and waterproof grade. It adapts to open-air and humid industrial sites. It effectively prevents dust and moisture from invading internal precision components.
-
Multi-Protocol System Compatibility: Supports standard Modbus RTU/ASCII industrial communication protocols. It seamlessly connects with PLC, DCS and industrial monitoring platforms. It realizes remote data viewing and equipment status monitoring.
-
Low Maintenance & Long Service Life: No mechanical moving parts and anti-aging circuit design reduce failure rate. It supports 7×24-hour full-load continuous operation. It lowers enterprise safety equipment operation and maintenance costs.
3. Detailed Segmented Technical Specifications
The GE RS-FS-9001 strictly complies with GE industrial manufacturing standards and international industrial safety monitoring specifications. All sensing performance, electrical indicators, structural parameters and environmental resistance capabilities pass professional laboratory testing and long-term field verification. The classified detailed parameters below support accurate model selection, engineering design and standardized batch procurement.
3.1 Basic Product & Application Parameters
The GE RS-FS-9001 is a high-reliability industrial UV flame detection probe. It focuses on real-time flame state monitoring and safety early warning for industrial combustion equipment.
-
Official Product Model: RS-FS-9001
-
Product Category: Industrial UV Flame Detector / Flame Monitoring Sensor Probe
-
Manufacturer: General Electric (GE)
-
Core Sensing Technology: Silicon Carbide (SiC) Ultraviolet (UV) Detection Technology
-
Core Functions: Real-time flame signal capture, flame intensity detection, abnormal flame alarm, 4-20mA signal output and remote data transmission
-
Applicable Equipment: Industrial boilers, combustion furnaces, power generation combustion equipment and petrochemical burning devices
-
Installation Method: 3/4-inch NPT female thread fixed installation, convenient for on-site assembly
-
Application Scenarios: Thermal power generation, petrochemical industry, industrial manufacturing boilers, flammable gas combustion systems and industrial safety fire monitoring system upgrading
-
Executive Standards: GE original factory specifications, industrial safety monitoring standards, ATEX, IECEx and ETL international explosion-proof safety certifications
3.2 Core Detection & Performance Parameters
High-precision sensing configuration and optimized detection algorithms ensure accurate and sensitive flame monitoring performance, meeting industrial safety supervision requirements.
-
Sensor Type: High-precision SiC ultraviolet professional flame sensor
-
Maximum Detection Distance: 15 meters long-distance stable flame detection
-
Detection Viewing Angle: 90° wide-angle coverage monitoring
-
Response Time: ≤10ms ultra-fast real-time response
-
Detection Accuracy: ±0.1% high-precision flame intensity identification
-
Output Signal: Standard industrial 4-20mA analog signal (proportional to flame intensity)
-
Wiring Mode: Two-wire current loop simplified wiring
-
MTBF Reliability: 500 million hours ultra-long stable operating cycle
3.3 Electrical & Communication Parameters
Stable electrical design and universal industrial communication configuration ensure seamless system docking and long-term stable signal transmission.
-
Rated Working Voltage: 24VDC standard industrial power supply
-
Communication Protocol: Modbus RTU / Modbus ASCII mainstream industrial protocols
-
Signal Stability: Low ripple signal output, strong anti-interference ability
-
System Compatibility: Fully compatible with GE industrial systems and mainstream PLC/DCS monitoring platforms
3.4 Mechanical & Dimension Parameters
Compact standardized structural design and threaded installation mode simplify on-site deployment and adapt to various industrial equipment installation environments.
-
Overall Dimensions: 120mm × 90mm × 50mm compact integrated size
-
Product Weight: 300g lightweight industrial design
-
Installation Interface: 3/4-inch NPT female threaded connector
-
Protection Grade: IP65/IP66 industrial dustproof and waterproof rating
-
Structural Feature: Integrated welded anti-loose and anti-disassembly structure
3.5 Environmental Adaptability Parameters
After strict extreme environment simulation testing, the detector maintains full-performance stable operation in various harsh industrial working conditions.
-
Full-Load Operating Temperature: -40°C to +85°C ultra-wide temperature stable operation
-
Working Humidity Range: 0%–95% RH non-condensing humid environment adaptation
-
Environmental Resistance: Resists mechanical vibration, industrial dust, moisture and strong electromagnetic interference
-
Continuous Operation Capacity: Supports 7×24-hour uninterrupted full-load industrial safety monitoring
3.6 Factory Testing & Quality Certification
Every GE RS-FS-9001 flame detector is manufactured under GE’s strict industrial quality control system. All units complete full-function testing and precision calibration before delivery to meet high-standard industrial safety monitoring requirements.
-
Core Testing Items: Sensing accuracy calibration, response speed test, signal stability test, high-low temperature cycle test and long-term aging test
-
Quality Inspection Standard: 100% full-function test + full performance calibration + complete test data filing
-
Authoritative Certification: ATEX, IECEx explosion-proof certification, ETL industrial safety certification and EMC electromagnetic compatibility certification
-
Field Operation Reliability: Widely deployed in global industrial safety monitoring projects with ultra-low false alarm rate and stable long-term performance
4. E-commerce Sales Mode & Complete Procurement Advantages
As a core safety monitoring device for industrial combustion systems, the GE RS-FS-9001 adopts standardized, transparent and efficient global industrial e-commerce sales mode. It focuses on industrial safety system maintenance, old flame detector upgrading and enterprise safety equipment strategic spare parts reserve. It provides one-stop standardized procurement and full-cycle professional technical services for industrial engineering integrators and petrochemical/power enterprises.
4.1 Standardized Transparent E-commerce System
All GE RS-FS-9001 products adopt unified original factory production and full-process standardized testing. The whole production, precision calibration and warehousing process is fully traceable. E-commerce platforms openly display complete product datasheets, performance test reports and official safety certification documents. Customers can verify product authenticity, detection accuracy and system matching performance online. This transparent sales mechanism effectively avoids refurbished and inferior detection probes. It fully guarantees the safety and stability of industrial flame monitoring systems.
4.2 Diversified Flexible Procurement Modes
Industrial safety equipment maintenance, daily spare parts stocking and large-scale safety system renovation have different procurement cycle and quantity demands. To cover all industrial application scenarios, we provide flexible multi-dimensional procurement solutions for the GE RS-FS-9001.
-
Emergency Spot Procurement: Suitable for on-site detector failure, aging damage and emergency replacement. Sufficient global spot inventory supports fast delivery. It helps enterprises quickly restore flame monitoring functions and avoid industrial safety hazards and production shutdown losses.
-
Small-Batch Spare Parts Stocking: Ideal for power plants, chemical enterprises and industrial factories to build safety equipment spare parts inventory. Pre-storing this high-reliability detector improves on-site fault emergency response speed and reduces system safety risks.
-
Large-Batch Engineering Procurement: Provide exclusive preferential pricing and long-term framework cooperation services for large-scale industrial safety system upgrading and combustion equipment renovation projects. It effectively reduces overall project procurement costs and shortens system commissioning cycles.
4.3 Full-Cycle After-Sales Service Guarantee
The flame detector is the key safety barrier of industrial combustion equipment. Its detection accuracy and operational stability directly affect enterprise production safety. We provide comprehensive full-cycle after-sales protection to eliminate all customer procurement risks.
-
100% Original Genuine Guarantee: All detectors are brand-new original GE products with complete factory test reports and safety qualification documents, ensuring 100% detection performance and system compatibility.
-
Professional Industrial Packaging: Adopt multi-layer anti-collision, shockproof, moisture-proof and dust-proof industrial packaging. It protects internal precision sensing chips and circuits from damage during long-distance transportation and storage.
-
24/7 Professional Technical Support: Provide pre-sales model matching consultation, in-sales installation and debugging guidance, and after-sales fault diagnosis and performance calibration services.
-
Long-Term Official Warranty Service: Enjoy unified official warranty coverage. Free maintenance and replacement services are provided for non-human-induced quality faults to reduce enterprise safety equipment operation costs.
5. Main Industrial Application Scenarios
Relying on its high-sensitivity UV detection, ultra-fast response, strong anti-interference and explosion-proof safety performance, the GE RS-FS-9001 is widely used in core safety monitoring links of various industrial combustion systems.
-
Thermal Power Generation System: Applied to boiler flame real-time monitoring in power plants. It accurately identifies flame extinguishment and abnormal combustion. It supports timely safety linkage protection to ensure stable power generation operation.
-
Petrochemical Industrial Facilities: Serves as safety monitoring equipment for chemical combustion furnaces and reaction devices. It adapts to flammable and explosive harsh environments. It provides reliable fire risk early warning.
-
Industrial Boiler Combustion Equipment: Used in manufacturing industrial boilers and heating combustion systems. It realizes continuous flame state monitoring. It avoids equipment failure and safety accidents caused by abnormal combustion.
-
Old Safety Monitoring System Upgrading: Replaces low-precision, slow-response and high-false-alarm old detectors. It improves the overall safety monitoring level and operational stability of industrial combustion systems without large-scale equipment reconstruction.
6. Product Value & Market Competitiveness
The GE RS-FS-9001 solves common industry pain points of traditional flame detectors, such as slow response, low detection accuracy, easy interference and short service life. It integrates advanced SiC UV sensing technology, ultra-fast response mechanism, industrial explosion-proof design and stable signal output. It comprehensively improves the accuracy, stability and safety level of industrial flame monitoring systems.
In the global industrial safety spare parts e-commerce market, the GE RS-FS-9001 has outstanding differentiated competitiveness. It features ultra-long service life, low false alarm rate, wide environmental adaptability and international authoritative safety certification. Combined with standardized genuine procurement, complete qualification documents and full-cycle professional after-sales services, it is the preferred safety detection device for industrial combustion system maintenance, safety upgrading and enterprise strategic spare parts reserve.